Stainless steel finish can be permanently marked by carbon-steel contamination. Use segregated tools/abrasives and protect finished surfaces through fabrication and installation.
Home › Knowledge Hub › Metal Fabrication
GLOBALTEK ENGINEERING KNOWLEDGE HUB · ACTIVITY 19
Metal Fabrication
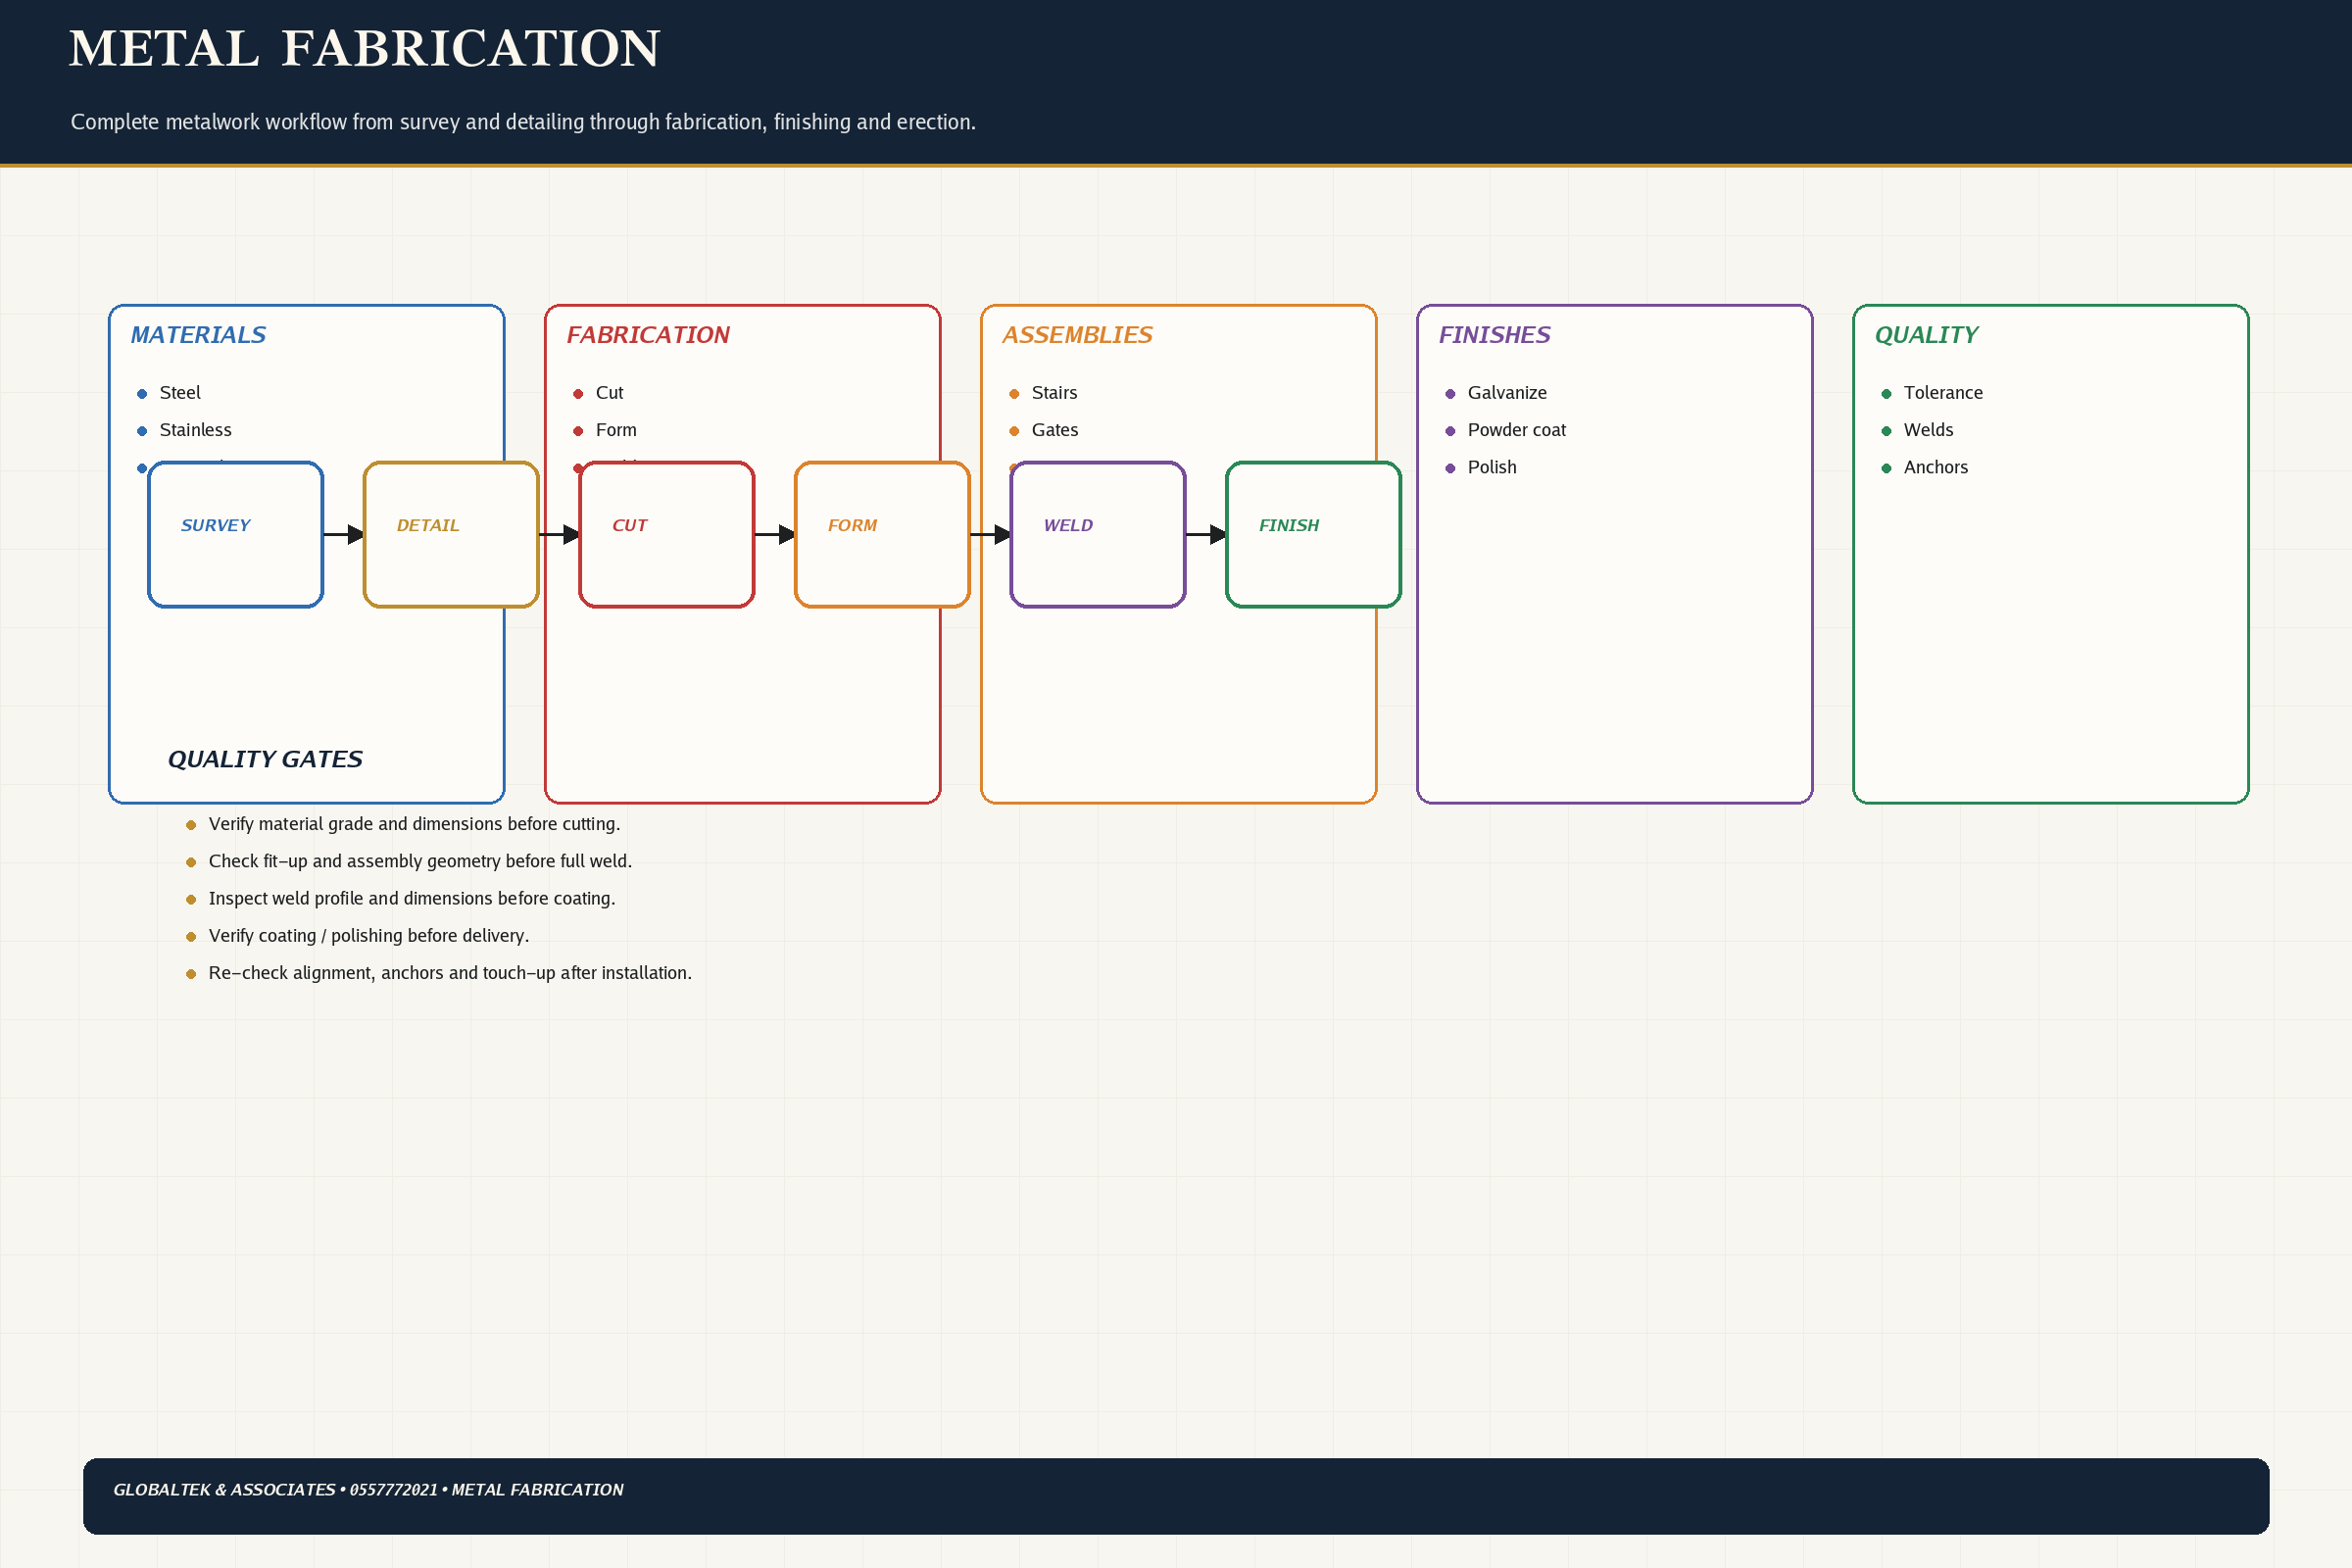
Metal fabrication turns drawings into load-carrying or decorative assemblies through cutting, forming, welding, machining, finishing and anchoring. Heat input, distortion, corrosion compatibility and installation tolerance must be controlled.

GUIDE MAP
Read the discipline visually, then go into the engineering detail.
Every image below is activity-specific. No repeated generic placeholder sheets are used in this guide.
01
System Overview
Metal fabrication covers structural / architectural frames, brackets, trims, screens, railings, furniture bases and decorative elements. The work combines engineering of loads / fixings with fabrication quality and finish control.
Open section →
02
Engineering Fundamentals
Verify material grade, thickness and finish requirement
Open section →
03
Execution Workflow
Verify dimensions, loads, anchors and visible joints
Open section →
04
Technical Chapters
27 individual sub-activity drawings with discipline-specific notes and inspection controls.
Open section →
05
QA/QC
Material grade / thickness match approved drawing
Open section →
06
Failure Analysis
Fabricating from architectural sketch without final shop dimensions
Open section →
07
Maintenance
Clean stainless / decorative metal with compatible non-abrasive products
Open section →
08
Standards & Brands
Approved structural / fabrication drawings and calculations where load-bearing
Open section →01 · SYSTEM OVERVIEW
What this activity is
What this activity is
Metal fabrication covers structural / architectural frames, brackets, trims, screens, railings, furniture bases and decorative elements. The work combines engineering of loads / fixings with fabrication quality and finish control.
What to expect
Expect fabricated metal to require accurate shop drawings and finish samples before production. Weld locations, visible joints, tolerances, anchors and finish direction must be agreed because grinding or site touch-up can change appearance.
01Verify material grade, thickness and finish requirement
02Use fabrication drawings with weld/connection details and datums
03Control jigs, fit-up and heat distortion during welding
04Grind/polish only to the specified finish without reducing critical section
05Apply compatible corrosion protection/coating
06Install with engineered anchors and allow final alignment
02 · ENGINEERING FUNDAMENTALS
Understand why the system behaves the way it does.
01
Weld size/length and connection capacity require engineering design for structural actions; decorative appearance is not proof of capacity
02
Thermal distortion increases with uneven heat input and restraint; sequence and balanced welding reduce distortion
03
Galvanic compatibility matters when dissimilar metals are connected in wet/exterior conditions
Weld symbols on drawings should define weld type, size, length and location; fabricators should not infer structural weld requirements from appearance.
Anchors are part of the connection system. Hole cleaning, embedment, edge distance, torque/cure and base-material condition can be as important as nominal anchor diameter.
03 · EXECUTION WORKFLOW
Six progressive stages from preparation to verified handover.
Open any plate to read the full-resolution technical notes.
01Survey Shopdrawings 02Cutting Forming
 03Fitup Welding
 04Grinding Finishing
 05Site Erection
 06Inspection Handover
STAGE 01
Survey Shopdrawings
Verify dimensions, loads, anchors and visible joints
Engineering intent
Confirm steel / stainless / aluminium grade and thickness before fabrication
Inspection / hold point
Material grade / thickness match approved drawing
Best practice
Use jigs for repeatability
Failure to avoid
Fabricating from architectural sketch without final shop dimensions
Handover / maintenance
Clean stainless / decorative metal with compatible non-abrasive products
STAGE 02
Cutting Forming
Cut, laser, drill, bend and machine to controlled dimensions
Engineering intent
Procedure, fit-up, heat control and finishing appropriate to visible / structural requirement
Inspection / hold point
Geometry and dimensions are verified in factory
Best practice
Trial-assemble complex frames in factory
Failure to avoid
Excessive welding causing distortion
Handover / maintenance
Repair coating damage before corrosion spreads
STAGE 03
Fitup Welding
Set geometry and trial-fit parts before final welding
Engineering intent
Sequence welding and provide jigs / restraint to control movement
Inspection / hold point
Welds / joints meet visual or structural acceptance requirement
Best practice
Separate grinding tools for stainless to avoid contamination
Failure to avoid
Grinding visible stainless inconsistently
Handover / maintenance
Check exposed anchors / joints in high-vibration or external locations
STAGE 04
Grinding Finishing
Execute controlled welds and finish visible joints to approved standard
Engineering intent
Select primer / galvanizing / stainless grade to exposure
Inspection / hold point
Finish colour / grain / sheen matches sample
Best practice
Protect finished metal with removable film / wrapping during transport
Failure to avoid
Site-welding after final powder coat without proper repair system
Handover / maintenance
Avoid chloride-rich cleaners on susceptible stainless grades
STAGE 05
Site Erection
Prepare and apply polish, powder coat, paint, PVD or protection
Engineering intent
Coordinate brushed / polished grain direction across adjacent pieces
Inspection / hold point
Anchors / fixings match design and substrate
Best practice
Design fixings for adjustment and future access
Failure to avoid
Using anchors without verifying substrate / edge distance
Handover / maintenance
Maintain moving metal hardware / pivots according to manufacturer guidance
STAGE 06
Inspection Handover
Set levels, drill / anchor safely, isolate dissimilar metals and protect final finish
Engineering intent
Design for load, substrate, edge distance and access
Inspection / hold point
Installed work is plumb / level / protected and free from corrosion contamination
Best practice
Approve finish sample under final lighting
Failure to avoid
Mixing carbon-steel contamination onto stainless surfaces
Handover / maintenance
Protect decorative metal during adjacent abrasive maintenance
04 · TECHNICAL CHAPTERS
27 detailed sub-activities for Metal Fabrication.
The file naming and page mapping are one-to-one: each technical subject has its own individual high-resolution image.
01Material Selection02Sections Plates03Laser Plasma Cutting04Drilling Holes Slots05Bending Pressbrake06Rolling Curving07Welding Processes08Weld Joints Symbols09Fitup Tacking10Distortion Control11Grinding Weld Blending12Stainless Polishing13Staircases14Handrails Balustrades15Gates Doors16Canopies Frames17Brackets Supports18Baseplates Anchors19Hotdip Galvanizing20Powder Coating21Stainless Finishes22Dissimilar Metal Isolation23Fabrication Tolerances24Shopdrawings Bom25Site Erection26Bolted Connections27Inspection NDT
TECHNICAL CHAPTER 01
Material Selection
Material Selection: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for material selection before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Material grade / thickness match approved drawing
Failure to avoid
Fabricating from architectural sketch without final shop dimensions
Maintenance / long-term performance
Clean stainless / decorative metal with compatible non-abrasive products

TECHNICAL CHAPTER 02
Sections Plates
Sections Plates: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for sections plates before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Geometry and dimensions are verified in factory
Failure to avoid
Excessive welding causing distortion
Maintenance / long-term performance
Repair coating damage before corrosion spreads

TECHNICAL CHAPTER 03
Laser Plasma Cutting
Laser Plasma Cutting: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for laser plasma cutting before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Welds / joints meet visual or structural acceptance requirement
Failure to avoid
Grinding visible stainless inconsistently
Maintenance / long-term performance
Check exposed anchors / joints in high-vibration or external locations

TECHNICAL CHAPTER 04
Drilling Holes Slots
Drilling Holes Slots: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for drilling holes slots before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Finish colour / grain / sheen matches sample
Failure to avoid
Site-welding after final powder coat without proper repair system
Maintenance / long-term performance
Avoid chloride-rich cleaners on susceptible stainless grades

TECHNICAL CHAPTER 05
Bending Pressbrake
Bending Pressbrake: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for bending pressbrake before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Anchors / fixings match design and substrate
Failure to avoid
Using anchors without verifying substrate / edge distance
Maintenance / long-term performance
Maintain moving metal hardware / pivots according to manufacturer guidance

TECHNICAL CHAPTER 06
Rolling Curving
Rolling Curving: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for rolling curving before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Installed work is plumb / level / protected and free from corrosion contamination
Failure to avoid
Mixing carbon-steel contamination onto stainless surfaces
Maintenance / long-term performance
Protect decorative metal during adjacent abrasive maintenance

TECHNICAL CHAPTER 07
Welding Processes
Welding Processes: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for welding processes before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Material grade / thickness match approved drawing
Failure to avoid
Fabricating from architectural sketch without final shop dimensions
Maintenance / long-term performance
Clean stainless / decorative metal with compatible non-abrasive products

TECHNICAL CHAPTER 08
Weld Joints Symbols
Weld Joints Symbols: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for weld joints symbols before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Geometry and dimensions are verified in factory
Failure to avoid
Excessive welding causing distortion
Maintenance / long-term performance
Repair coating damage before corrosion spreads

TECHNICAL CHAPTER 09
Fitup Tacking
Fitup Tacking: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for fitup tacking before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Welds / joints meet visual or structural acceptance requirement
Failure to avoid
Grinding visible stainless inconsistently
Maintenance / long-term performance
Check exposed anchors / joints in high-vibration or external locations

TECHNICAL CHAPTER 10
Distortion Control
Distortion Control: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for distortion control before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Finish colour / grain / sheen matches sample
Failure to avoid
Site-welding after final powder coat without proper repair system
Maintenance / long-term performance
Avoid chloride-rich cleaners on susceptible stainless grades

TECHNICAL CHAPTER 11
Grinding Weld Blending
Grinding Weld Blending: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for grinding weld blending before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Anchors / fixings match design and substrate
Failure to avoid
Using anchors without verifying substrate / edge distance
Maintenance / long-term performance
Maintain moving metal hardware / pivots according to manufacturer guidance

TECHNICAL CHAPTER 12
Stainless Polishing
Stainless Polishing: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for stainless polishing before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Installed work is plumb / level / protected and free from corrosion contamination
Failure to avoid
Mixing carbon-steel contamination onto stainless surfaces
Maintenance / long-term performance
Protect decorative metal during adjacent abrasive maintenance

TECHNICAL CHAPTER 13
Staircases
Staircases: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for staircases before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Material grade / thickness match approved drawing
Failure to avoid
Fabricating from architectural sketch without final shop dimensions
Maintenance / long-term performance
Clean stainless / decorative metal with compatible non-abrasive products

TECHNICAL CHAPTER 14
Handrails Balustrades
Handrails Balustrades: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for handrails balustrades before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Geometry and dimensions are verified in factory
Failure to avoid
Excessive welding causing distortion
Maintenance / long-term performance
Repair coating damage before corrosion spreads

TECHNICAL CHAPTER 15
Gates Doors
Gates Doors: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for gates doors before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Welds / joints meet visual or structural acceptance requirement
Failure to avoid
Grinding visible stainless inconsistently
Maintenance / long-term performance
Check exposed anchors / joints in high-vibration or external locations

TECHNICAL CHAPTER 16
Canopies Frames
Canopies Frames: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for canopies frames before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Finish colour / grain / sheen matches sample
Failure to avoid
Site-welding after final powder coat without proper repair system
Maintenance / long-term performance
Avoid chloride-rich cleaners on susceptible stainless grades

TECHNICAL CHAPTER 17
Brackets Supports
Brackets Supports: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for brackets supports before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Anchors / fixings match design and substrate
Failure to avoid
Using anchors without verifying substrate / edge distance
Maintenance / long-term performance
Maintain moving metal hardware / pivots according to manufacturer guidance

TECHNICAL CHAPTER 18
Baseplates Anchors
Baseplates Anchors: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for baseplates anchors before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Installed work is plumb / level / protected and free from corrosion contamination
Failure to avoid
Mixing carbon-steel contamination onto stainless surfaces
Maintenance / long-term performance
Protect decorative metal during adjacent abrasive maintenance

TECHNICAL CHAPTER 19
Hotdip Galvanizing
Hotdip Galvanizing: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for hotdip galvanizing before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Material grade / thickness match approved drawing
Failure to avoid
Fabricating from architectural sketch without final shop dimensions
Maintenance / long-term performance
Clean stainless / decorative metal with compatible non-abrasive products

TECHNICAL CHAPTER 20
Powder Coating
Powder Coating: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for powder coating before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Geometry and dimensions are verified in factory
Failure to avoid
Excessive welding causing distortion
Maintenance / long-term performance
Repair coating damage before corrosion spreads

TECHNICAL CHAPTER 21
Stainless Finishes
Stainless Finishes: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for stainless finishes before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Welds / joints meet visual or structural acceptance requirement
Failure to avoid
Grinding visible stainless inconsistently
Maintenance / long-term performance
Check exposed anchors / joints in high-vibration or external locations

TECHNICAL CHAPTER 22
Dissimilar Metal Isolation
Dissimilar Metal Isolation: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for dissimilar metal isolation before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Finish colour / grain / sheen matches sample
Failure to avoid
Site-welding after final powder coat without proper repair system
Maintenance / long-term performance
Avoid chloride-rich cleaners on susceptible stainless grades

TECHNICAL CHAPTER 23
Fabrication Tolerances
Fabrication Tolerances: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for fabrication tolerances before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Anchors / fixings match design and substrate
Failure to avoid
Using anchors without verifying substrate / edge distance
Maintenance / long-term performance
Maintain moving metal hardware / pivots according to manufacturer guidance

TECHNICAL CHAPTER 24
Shopdrawings Bom
Shopdrawings Bom: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for shopdrawings bom before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Installed work is plumb / level / protected and free from corrosion contamination
Failure to avoid
Mixing carbon-steel contamination onto stainless surfaces
Maintenance / long-term performance
Protect decorative metal during adjacent abrasive maintenance

TECHNICAL CHAPTER 25
Site Erection
Site Erection: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for site erection before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Material grade / thickness match approved drawing
Failure to avoid
Fabricating from architectural sketch without final shop dimensions
Maintenance / long-term performance
Clean stainless / decorative metal with compatible non-abrasive products

TECHNICAL CHAPTER 26
Bolted Connections
Bolted Connections: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for bolted connections before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Geometry and dimensions are verified in factory
Failure to avoid
Excessive welding causing distortion
Maintenance / long-term performance
Repair coating damage before corrosion spreads

TECHNICAL CHAPTER 27
Inspection NDT
Inspection NDT: Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Design intent
Define the performance and construction intent for inspection ndt before fabrication or installation. Read the drawing together with the approved project specification, manufacturer data and adjoining details.
Coordination
Coordinate material grade, cutting/forming, fit-up, welding, distortion, grinding, anchors/bolts, corrosion protection, finishing, tolerances, erection and inspection/NDT.
Inspection / QA
Welds / joints meet visual or structural acceptance requirement
Failure to avoid
Grinding visible stainless inconsistently
Maintenance / long-term performance
Check exposed anchors / joints in high-vibration or external locations
05 · QA/QC
Inspect before concealment and before handover.
01Material grade / thickness match approved drawing
02Geometry and dimensions are verified in factory
03Welds / joints meet visual or structural acceptance requirement
04Finish colour / grain / sheen matches sample
05Anchors / fixings match design and substrate
06Installed work is plumb / level / protected and free from corrosion contamination
06 · COMMON FAILURES
Recognise the failure mechanism—not only the visible defect.
Failures to avoid
×Fabricating from architectural sketch without final shop dimensions
×Excessive welding causing distortion
×Grinding visible stainless inconsistently
×Site-welding after final powder coat without proper repair system
×Using anchors without verifying substrate / edge distance
×Mixing carbon-steel contamination onto stainless surfaces
07 · MAINTENANCE & AFTERCARE
Design for access, repair and long-term performance.
Maintenance controls
✓Clean stainless / decorative metal with compatible non-abrasive products
✓Repair coating damage before corrosion spreads
✓Check exposed anchors / joints in high-vibration or external locations
✓Avoid chloride-rich cleaners on susceptible stainless grades
✓Maintain moving metal hardware / pivots according to manufacturer guidance
✓Protect decorative metal during adjacent abrasive maintenance
08 · STANDARDS & MANUFACTURER REFERENCES
Use the latest approved project documents and tested systems.
• Approved structural / fabrication drawings and calculations where load-bearing
• Relevant EN / AWS / ASTM welding / material standards referenced by project
• Coating / galvanizing / powder-coating manufacturer specifications
• Anchor manufacturer design and installation requirements
• Project architectural finish sample / direction / sheen requirements
• Inspection / NDT requirements where specified by structural engineer / contract
Technical guidance is educational and indicative. Final design, dimensions, materials, installation details and acceptance criteria must follow the approved project documents, manufacturer instructions and the latest requirements of the relevant UAE authority, landlord, consultant and specialist engineer.
09 · COMPLETE IMAGE LIBRARY
40 high-resolution visuals assigned to this activity.
Each file remains separate and is mapped directly to its relevant section. Click any image to inspect it at full resolution.
HeroOverviewFundamentalsQA/QCFailuresMaintenanceStandards & Brands Stage 01 · Survey ShopdrawingsStage 02 · Cutting FormingStage 03 · Fitup WeldingStage 04 · Grinding FinishingStage 05 · Site ErectionStage 06 · Inspection Handover 01 · Material Selection02 · Sections Plates03 · Laser Plasma Cutting04 · Drilling Holes Slots05 · Bending Pressbrake06 · Rolling Curving07 · Welding Processes08 · Weld Joints Symbols09 · Fitup Tacking10 · Distortion Control11 · Grinding Weld Blending12 · Stainless Polishing13 · Staircases14 · Handrails Balustrades15 · Gates Doors16 · Canopies Frames17 · Brackets Supports18 · Baseplates Anchors19 · Hotdip Galvanizing20 · Powder Coating21 · Stainless Finishes22 · Dissimilar Metal Isolation23 · Fabrication Tolerances24 · Shopdrawings Bom25 · Site Erection26 · Bolted Connections27 · Inspection NDT